Mist Eliminator Selection for Wet Scrubber Systems
2026-09-23
Mist Eliminator Selection for Wet Scrubber Systems is not a one-variable purchasing decision. In industrial air-pollution-control and waste-gas treatment projects, material choice, equipment settings, operating conditions and downstream construction interact. A specification that lists only a product name or one headline value can leave important risks unresolved. This guide organizes the questions that buyers, engineers and suppliers should review before approving a trial or production order.
The aim is not to prescribe one universal design. Different applications can justify different limits, and final performance often depends on the complete system. Use the following framework to define service conditions, request comparable evidence and validate a representative finished article. Do not treat general guidance as a substitute for project-specific engineering, safety or regulatory review.
Define the Carryover Problem
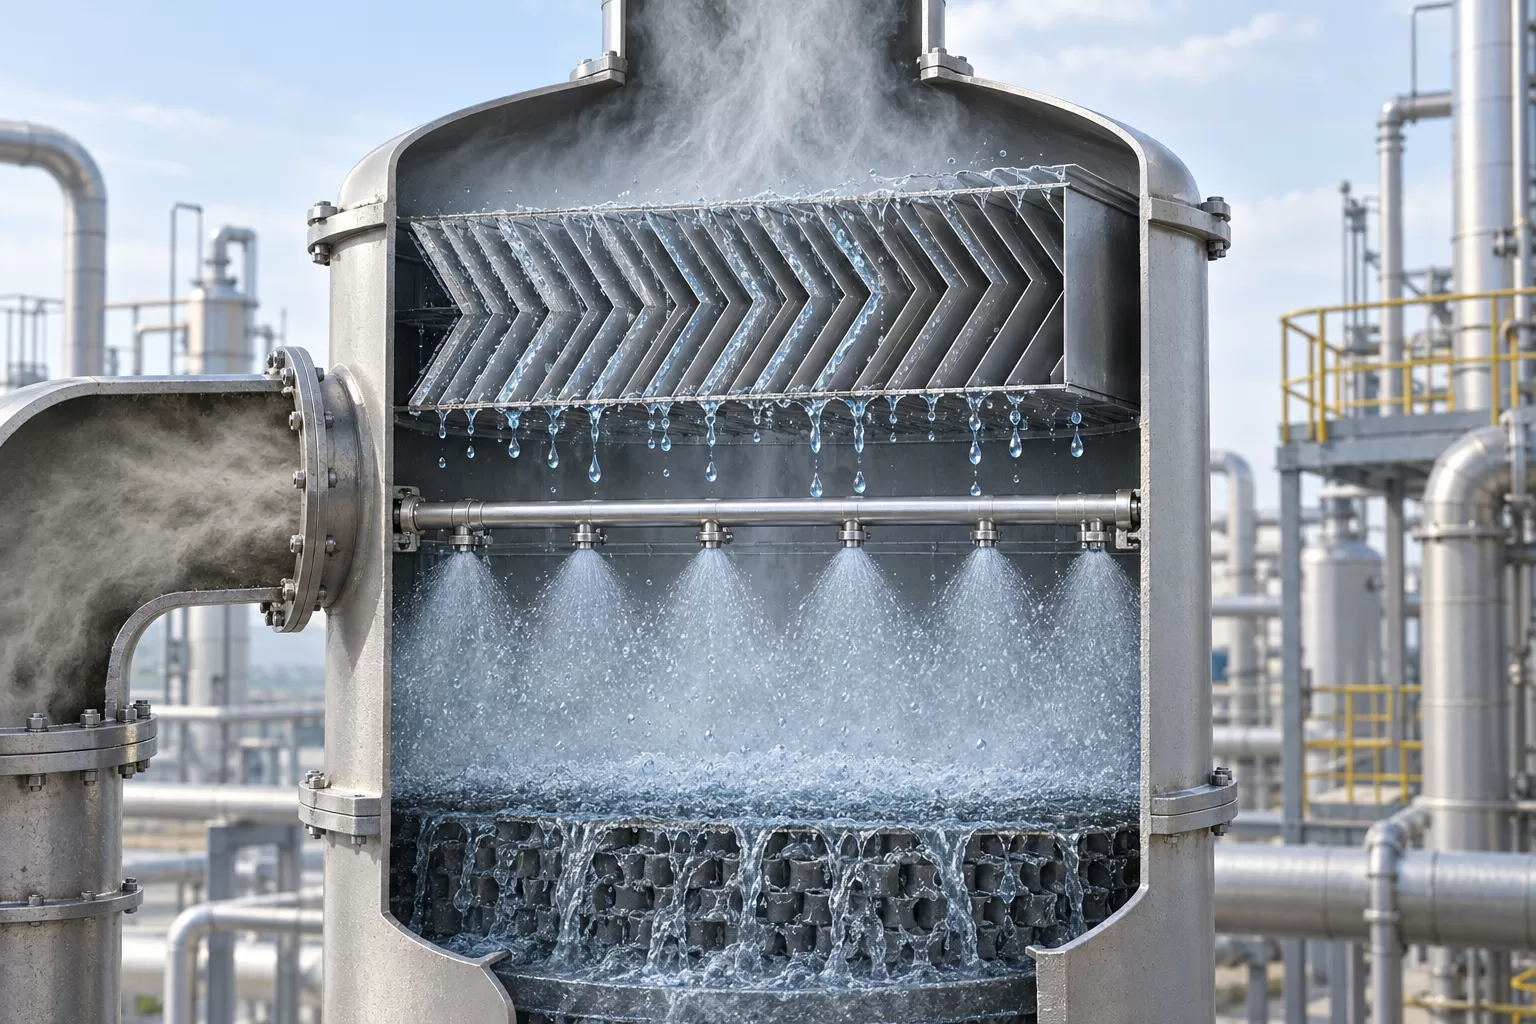
Mist leaving a scrubber can contain process chemicals or dissolved solids and may damage downstream fans, ducts or stacks. For project teams, this point should be converted into a written requirement rather than left as an informal expectation. Consider normal production, startup, shutdown, cleaning, storage and foreseeable upset conditions, because the most demanding combination may not appear during a short demonstration.
Identify liquid chemistry, expected droplet distribution, gas flow range and acceptable carryover at the actual sampling boundary. Ask the supplier to state the method, sample preparation, tolerance, inspection frequency and action taken when a result drifts. When finished-system performance is involved, confirm it with a representative production trial and keep the approved sample and records for later lot comparison.
Match Type to Droplet and Fouling Behavior
Mesh pads, vane packs and other separators differ in capture mechanism, pressure drop, drainage and tolerance for sticky or crystallizing deposits. The practical risk is that a single laboratory value may not represent production variation, installation details or real operating conditions. Consider normal production, startup, shutdown, cleaning, storage and foreseeable upset conditions, because the most demanding combination may not appear during a short demonstration.
Compare options using vendor performance data at the expected density, viscosity, solids content and turndown rather than choosing by face velocity alone. Ask the supplier to state the method, sample preparation, tolerance, inspection frequency and action taken when a result drifts. When finished-system performance is involved, confirm it with a representative production trial and keep the approved sample and records for later lot comparison.
Control Velocity and Distribution
Local high velocity caused by poor inlet distribution can re-entrain droplets even when the average vessel velocity appears acceptable. A useful specification connects the intended service condition to evidence that both buyer and supplier can review consistently. Consider normal production, startup, shutdown, cleaning, storage and foreseeable upset conditions, because the most demanding combination may not appear during a short demonstration.
Review vessel transitions, open area, support frames and drain paths, and confirm performance at minimum and maximum operating flow. Ask the supplier to state the method, sample preparation, tolerance, inspection frequency and action taken when a result drifts. When finished-system performance is involved, confirm it with a representative production trial and keep the approved sample and records for later lot comparison.
Plan Washing and Drainage
A separator that captures droplets but cannot drain or be cleaned predictably will accumulate deposits and lose performance. This is also a communication issue: design, purchasing, production and maintenance teams should use the same definitions. Consider normal production, startup, shutdown, cleaning, storage and foreseeable upset conditions, because the most demanding combination may not appear during a short demonstration.
Provide access, wash coverage, compatible materials and a drainage route that prevents flooding or liquid being pulled back into the gas stream. Ask the supplier to state the method, sample preparation, tolerance, inspection frequency and action taken when a result drifts. When finished-system performance is involved, confirm it with a representative production trial and keep the approved sample and records for later lot comparison.
Monitor Condition in Service
Increasing pressure drop, visible stack plume or downstream corrosion can indicate fouling, damage or poor drainage, but each symptom has multiple possible causes. For project teams, this point should be converted into a written requirement rather than left as an informal expectation. Consider normal production, startup, shutdown, cleaning, storage and foreseeable upset conditions, because the most demanding combination may not appear during a short demonstration.
Set inspection and cleaning triggers using pressure, operating history and visual evidence, then record findings to refine the maintenance interval. Ask the supplier to state the method, sample preparation, tolerance, inspection frequency and action taken when a result drifts. When finished-system performance is involved, confirm it with a representative production trial and keep the approved sample and records for later lot comparison.
Building a Reliable Procurement Brief
A good procurement brief for industrial air-pollution-control and waste-gas treatment projects should identify the application, operating envelope, interfaces, required evidence and acceptance process. It should also separate mandatory criteria from preferences. This makes supplier responses easier to compare and prevents an attractive but incomplete data sheet from becoming the only basis for a technical decision.
Before release, review the brief with the people who will process, install, operate and maintain the product or equipment. Resolve ambiguous terms, name the reference standards and agree how deviations will be handled. A small, well-documented trial usually provides more useful evidence than a large order based on assumptions.
Conclusion
Jiangsu Zhongkang Environmental recommends matching specifications to the real application and confirming critical points through representative samples or trials. Buyers should evaluate complete-system behavior, process consistency, traceability and maintainability alongside nominal specifications. This disciplined approach supports clearer quotations, smoother approvals and fewer surprises during production or operation without relying on unsupported performance claims.